

Tooling Solutions
We provide high-precision tooling solutions for five major sectors: automotive, medical, consumer electronics, packaging, industrial and other industries.
Exterior Trim‑Automotive
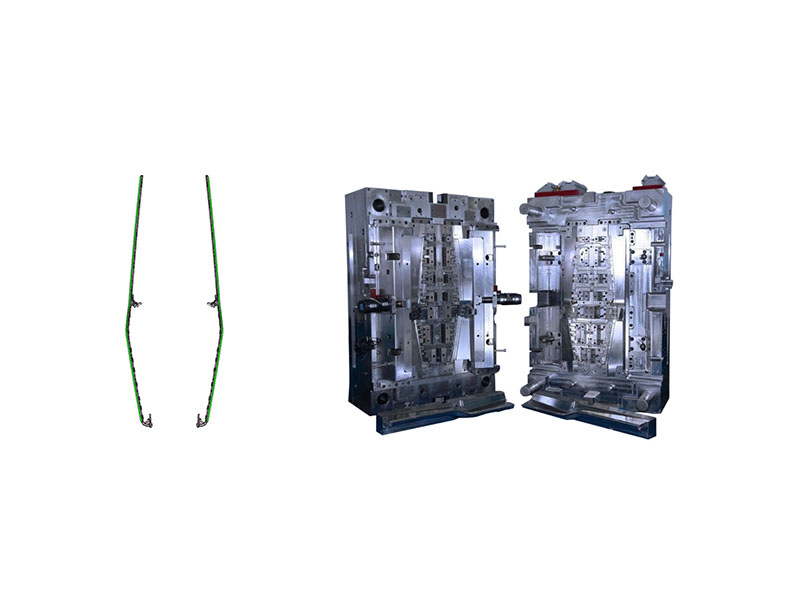
Light‑guide Bracket
-Cavity quantity: 1+1
-Cycle time: 100s
-Part length: 1000 mm
-Two‑color mold: No mold rotation or mold‑opening is required. After injection‑molding the hard material, the second‑shot injection can be carried out directly.
-Cycle time: 100s
-Part length: 1000 mm
-Two‑color mold: No mold rotation or mold‑opening is required. After injection‑molding the hard material, the second‑shot injection can be carried out directly.
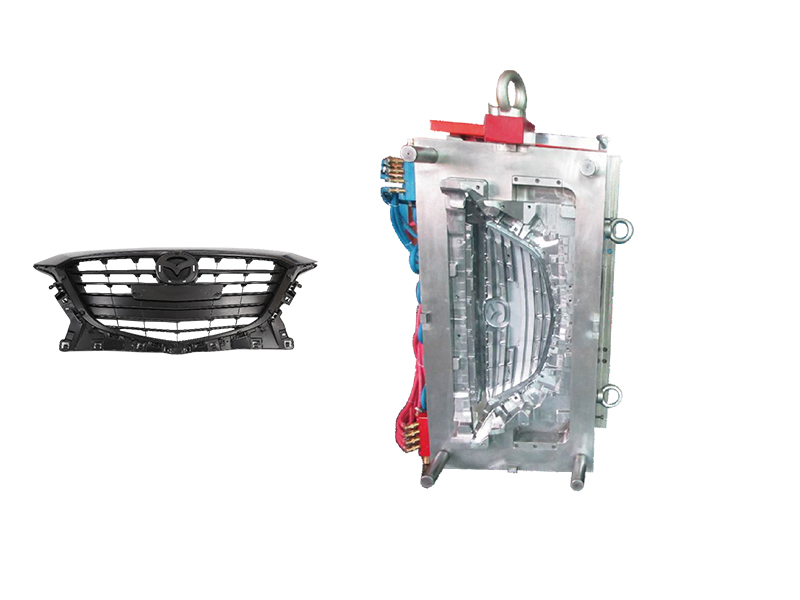
Air intake grille
-Cavity quantity: 1×1
-Cycle time: 57s
-Part size: 1150*425*235
-Boasting an integrated large curved shape, this Class‑A exterior surface demands flawless continuous light reflection.
-Cycle time: 57s
-Part size: 1150*425*235
-Boasting an integrated large curved shape, this Class‑A exterior surface demands flawless continuous light reflection.
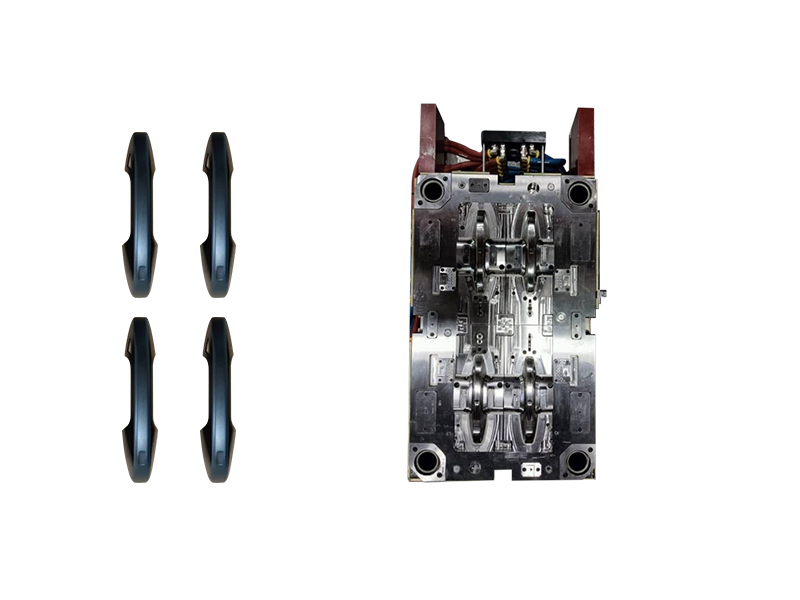
Door handle
-Cavity quantity: 1×4
-Cycle time: 48s
-Part appearance: Zero‑weld‑line, no parting‑line visible
-Cycle time: 48s
-Part appearance: Zero‑weld‑line, no parting‑line visible
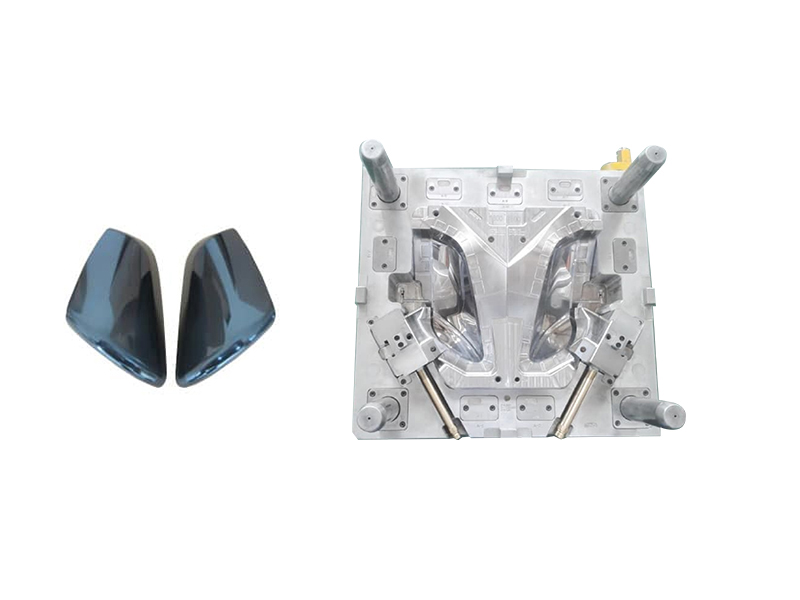
Rear-view Mirror
-Cavity quantity: 1+1
-Cycle time: 30s
-The rear‑view mirror part has multiple internal undercuts with limited space. Multiple parting actions are required for demolding. The cosmetic surface requires high‑gloss finish with mirror‑like effect and zero weld‑lines.
-Cycle time: 30s
-The rear‑view mirror part has multiple internal undercuts with limited space. Multiple parting actions are required for demolding. The cosmetic surface requires high‑gloss finish with mirror‑like effect and zero weld‑lines.
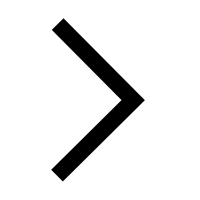
Interior Trim‑Automotive
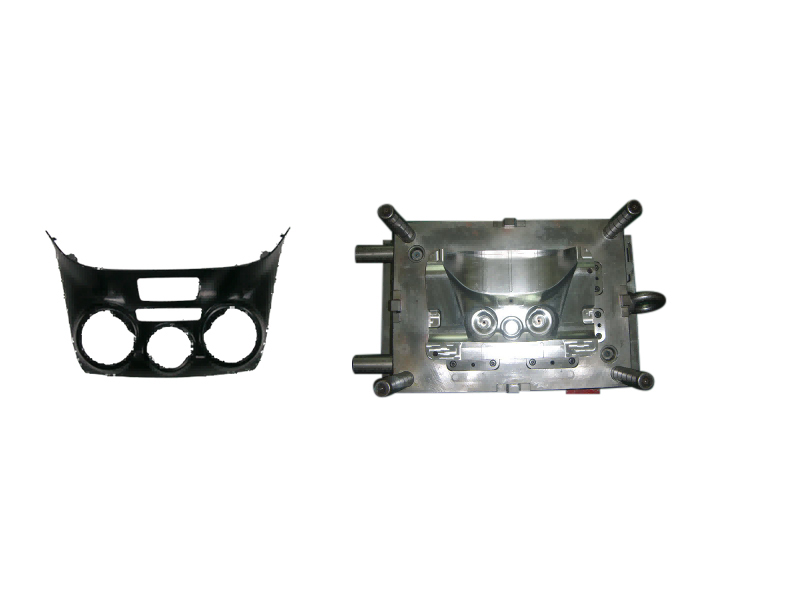
Instrument Panel system
-Cavity quantity: 1
-Cycle time: 40s
-This is a central‑control cover for Volkswagen. With multiple gates on the part, weld‑lines are prone to occur. Besides, it features complex structure and numerous undercuts, which may easily cause interferences.
-Cycle time: 40s
-This is a central‑control cover for Volkswagen. With multiple gates on the part, weld‑lines are prone to occur. Besides, it features complex structure and numerous undercuts, which may easily cause interferences.
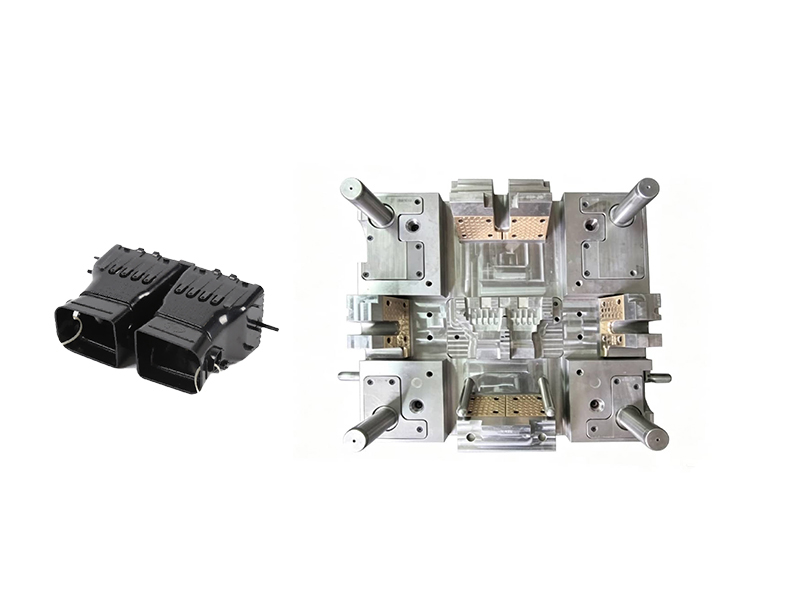
Air-conditioner vent
-Cavity quantity: 1
-Cycle time: 25s
-The air‑outlet housing has a complex structure with four‑side slides and lifters on the rear mold. The inner surface requires EDM texture with uniform grain finish, which will be machined by one‑piece copper electrode.
-Cycle time: 25s
-The air‑outlet housing has a complex structure with four‑side slides and lifters on the rear mold. The inner surface requires EDM texture with uniform grain finish, which will be machined by one‑piece copper electrode.
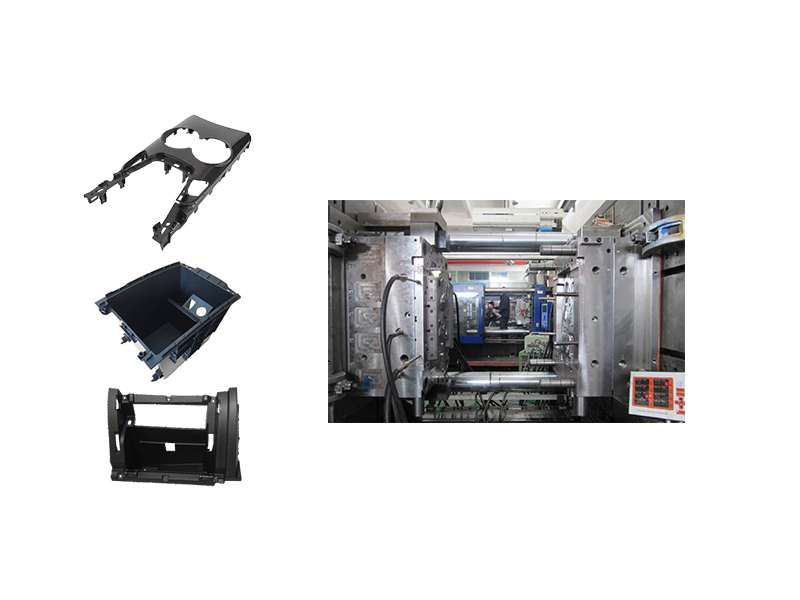
Armrest box Cup holder
-Cavity quantity: 1
-Cycle time: 50s
-The cup‑holder cover requires a high‑gloss cosmetic surface with zero weld‑lines. High‑mold‑temperature molding shall be adopted to avoid weld‑line defects.
-Cycle time: 50s
-The cup‑holder cover requires a high‑gloss cosmetic surface with zero weld‑lines. High‑mold‑temperature molding shall be adopted to avoid weld‑line defects.
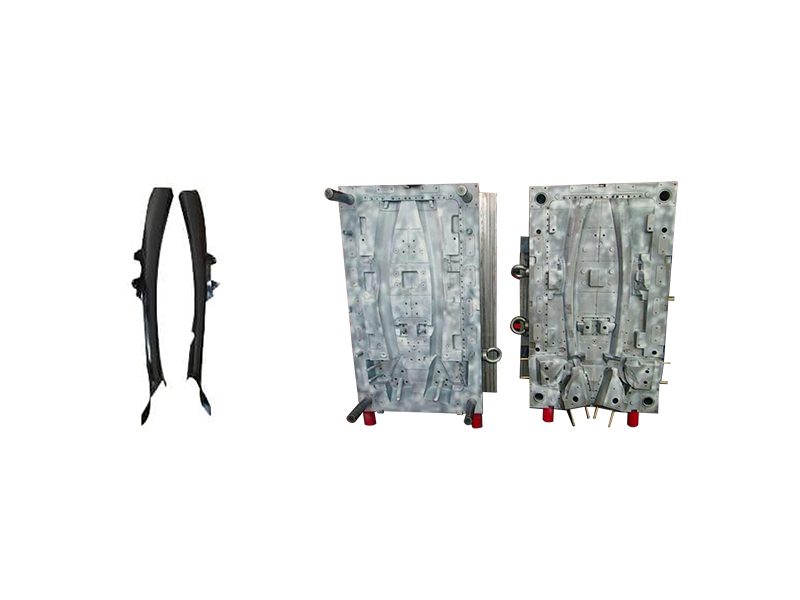
A-Pillar
-Cavity quantity: 1+1
-Cycle time: 60s
-This is a pillar part for Porsche. Its length exceeds 1.4 meters, and product deformation must be strictly controlled.
-Cycle time: 60s
-This is a pillar part for Porsche. Its length exceeds 1.4 meters, and product deformation must be strictly controlled.
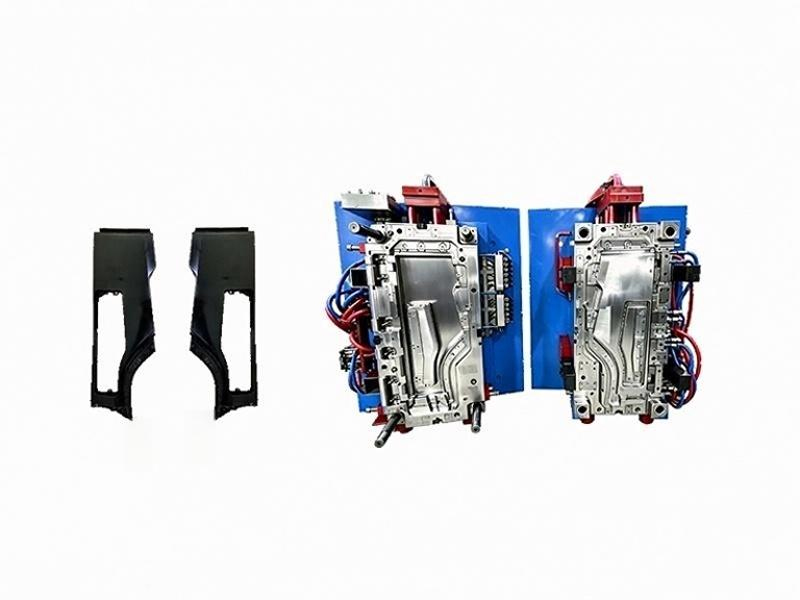
Inner fender Trim
-Cavity quantity: 1+1
-Cycle time: 72s
-The part requires spray‑painting on its cosmetic surface. Extremely high standards are demanded for machining and mold polishing. It shall be guaranteed that no shadow exists from all viewing angles and the surface finish is uniform.
-Cycle time: 72s
-The part requires spray‑painting on its cosmetic surface. Extremely high standards are demanded for machining and mold polishing. It shall be guaranteed that no shadow exists from all viewing angles and the surface finish is uniform.
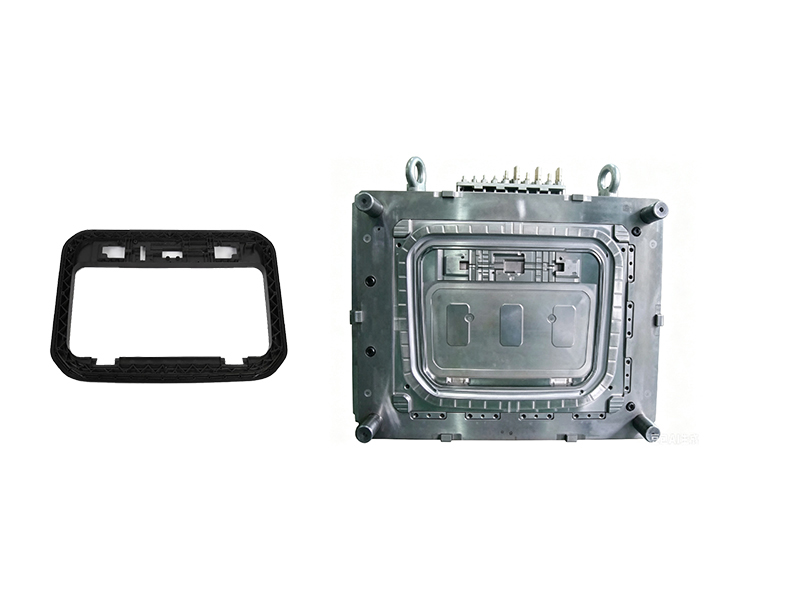
SUN roof
-Cavity quantity: 1×1
-Cycle time: 95s
-This part is a sun‑roof component. Flatness must be controlled, and sequential valve‑gating shall be adopted during filling to prevent deformation.
-Cycle time: 95s
-This part is a sun‑roof component. Flatness must be controlled, and sequential valve‑gating shall be adopted during filling to prevent deformation.
Functional & Structural Components
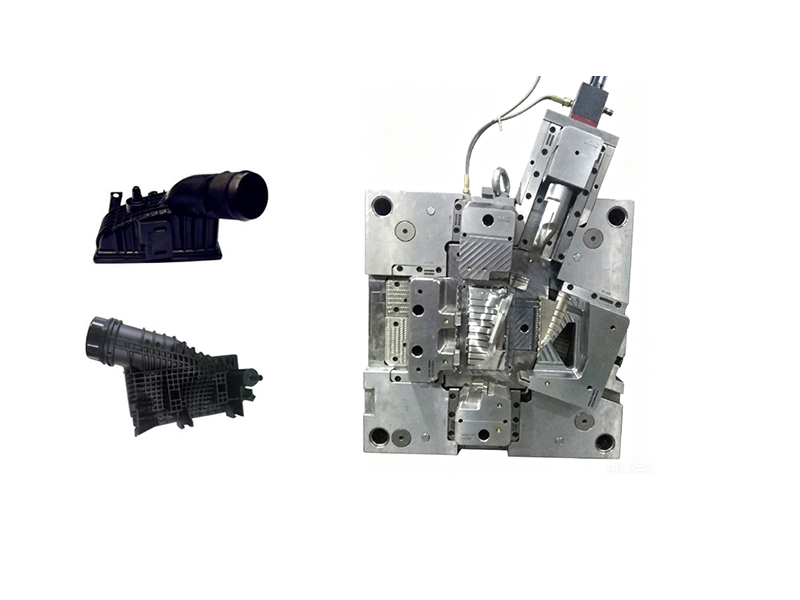
Valve&radiator tank
-Cavity quantity: 1×1
-Cycle time: 80s
-This radiator water tank belongs to Hanon system. Two separate parts need hot‑melting welding. The flatness requirement of the component is 0.8mm. Anti‑deformation structure and inserts shall be adopted to correct flatness.
-Cycle time: 80s
-This radiator water tank belongs to Hanon system. Two separate parts need hot‑melting welding. The flatness requirement of the component is 0.8mm. Anti‑deformation structure and inserts shall be adopted to correct flatness.
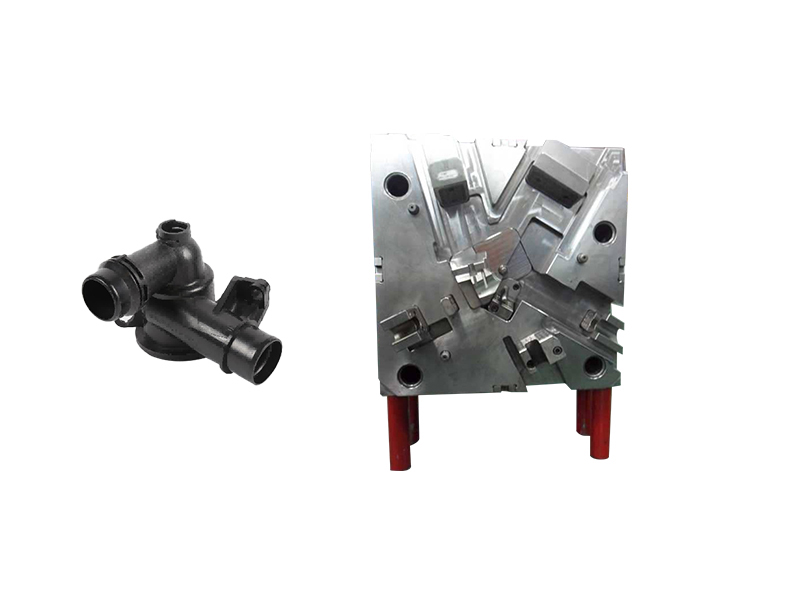
Precision joint/pipe fitting
-Cavity quantity: 1×1
-Cycle time: 40s
-The part has a complex structure. Mold‑opening and mold‑closing shall be carried out in sequence, and all movements are controlled by hydraulic cylinders.
-Cycle time: 40s
-The part has a complex structure. Mold‑opening and mold‑closing shall be carried out in sequence, and all movements are controlled by hydraulic cylinders.
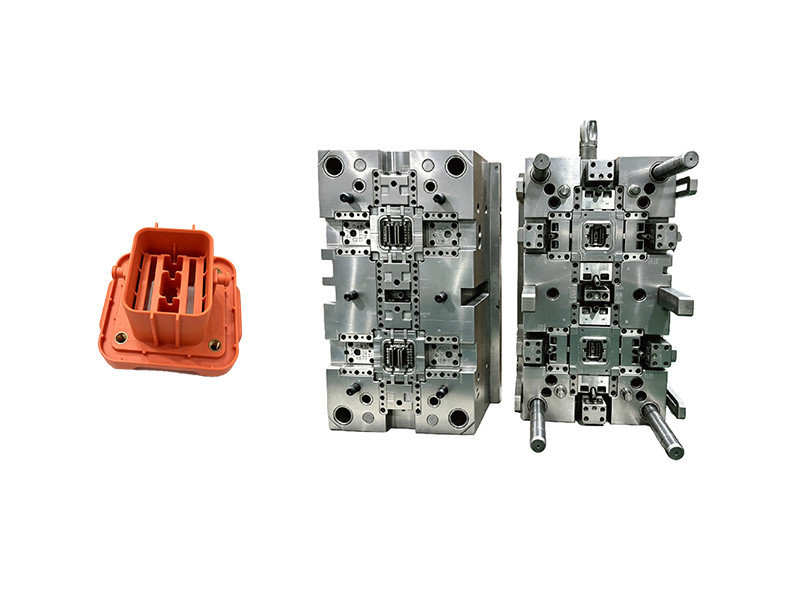
Connector
-Cavity quantity: 1×2
Molding cycle time: 66s
-The part features deep wall sections on the cavity side. A stripper‑plate structure is added to prevent the component from sticking to the cavity. Inner slides are installed on the cavity, adding extra mold‑opening movements.
-The part features deep wall sections on the cavity side. A stripper‑plate structure is added to prevent the component from sticking to the cavity. Inner slides are installed on the cavity, adding extra mold‑opening movements.
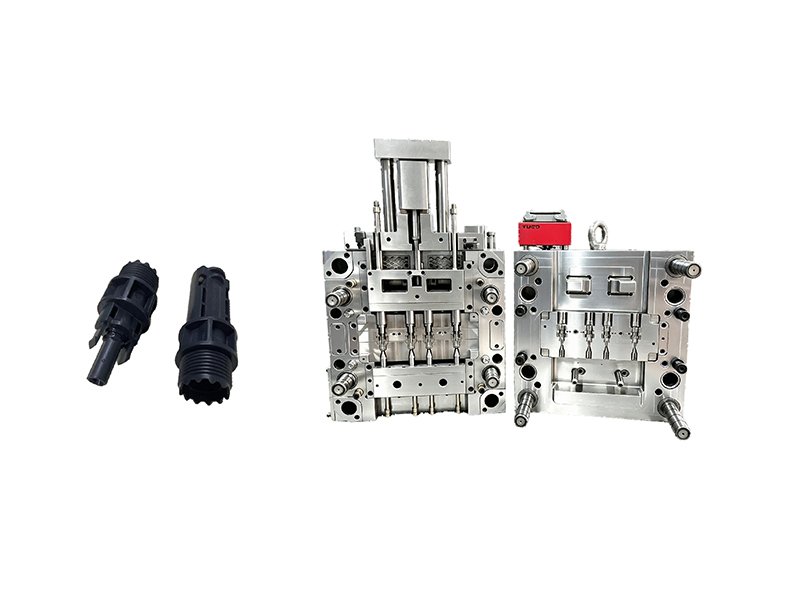
Connector
-Cavity quantity: 1×4
-Cycle time: 32s
-The part has thick wall sections. A full‑circle undercut of 0.45 mm exists at the internal terminal‑insert position, which requires forced ejection for demolding. No pull‑up deformation is allowed at the undercut area.
-Cycle time: 32s
-The part has thick wall sections. A full‑circle undercut of 0.45 mm exists at the internal terminal‑insert position, which requires forced ejection for demolding. No pull‑up deformation is allowed at the undercut area.
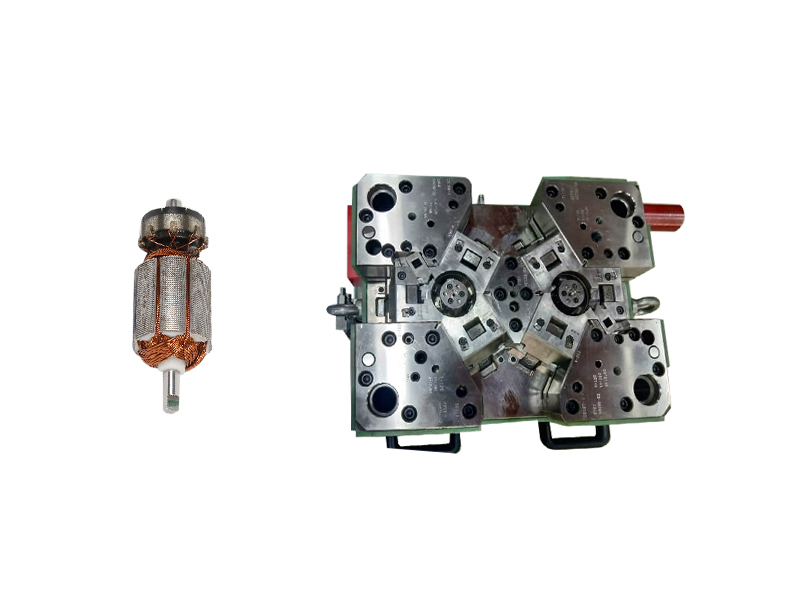
Mechatronic component
-Cavity quantity: 1×2
-Cycle time: 30s Mechatronic component‑brush part. Copper wires and steel inserts shall be placed for insert‑molding, and circularity must be guaranteed. -Extremely high‑precision requirements are imposed on positioning and installation of the metal hardware. The hardware parts shall be pre‑fixed by a pre‑shaping jig off‑machine before being loaded into the mold for injection molding.
-Cycle time: 30s Mechatronic component‑brush part. Copper wires and steel inserts shall be placed for insert‑molding, and circularity must be guaranteed. -Extremely high‑precision requirements are imposed on positioning and installation of the metal hardware. The hardware parts shall be pre‑fixed by a pre‑shaping jig off‑machine before being loaded into the mold for injection molding.
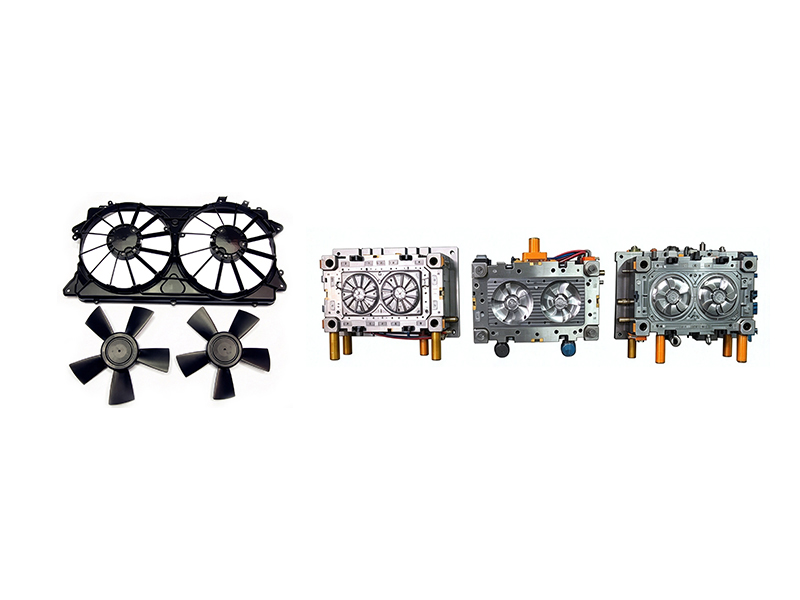
Fan
-Cycle time: 60s
-(1+1+1) T‑type mold
-Parts on the two parting sides are different. No stroke adjustment or double‑shot injection is required. Injection‑molding parameters for each side are controlled independently. Extra cooling is applied during single‑side waiting to achieve better product quality. ‑ The two molded parts can be assembled directly.